


Zhejiang Mingjia Environmental Protection Technology Co., Ltd. is a high-tech enterprise headquartered in Jiaxing, focusing on organic waste resource utilization. It independently develops core products including aerobic fermentation tanks and solid-liquid separators, holds 123 national patents, commands over 85% market share in Zhejiang Province, and exports to Europe, America, and Southeast Asia. With ISO and CE certification, Mingjia is dedicated to green circular solutions.
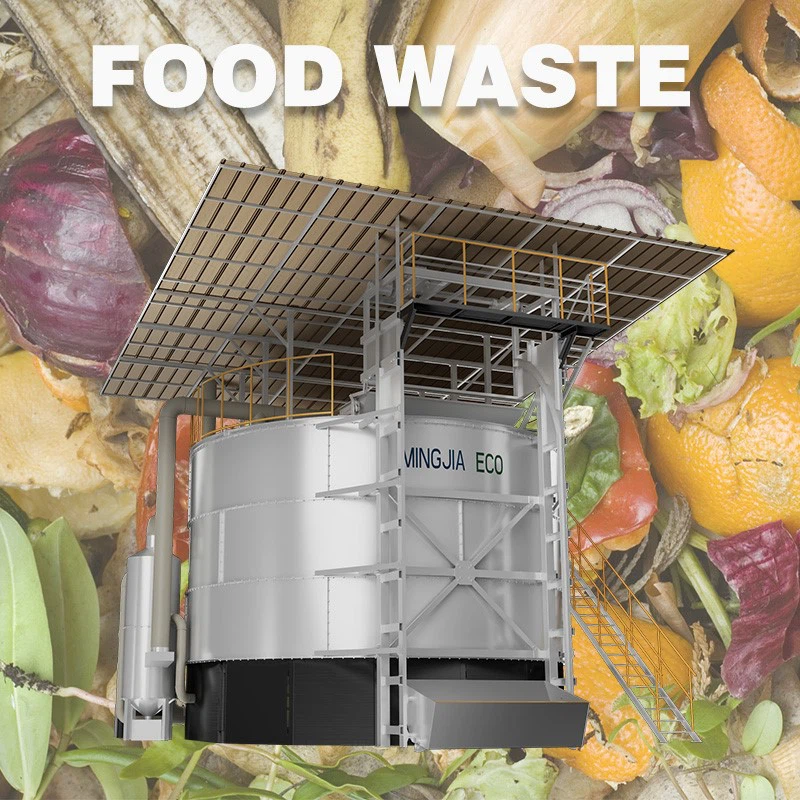
The Mingjia aerobic fermentation tank is an integrated, automated organic waste conversion system. It rapidly decomposes organic matter, kills harmful microorganisms, eliminates odors, and finally produces stable humus fertilizer to support ecological agriculture.
Models
| Model | 11FFG-55 | 11FFG-80 | 11FFG-100 | 11FFG-120 | 11FFG-140 | 11FFG-160 | 11FFG-220 | 11FFG-280 |
| Body Volume | 55m³ | 80m³ | 100m³ | 120m³ | 140m³ | 160m³ | 220m³ | 280m³ |
| Power | 29.25kW | 34.25kW | 39.25kW | 39.25kW | 43.75kW | 43.75kW | 84.25kW | 109.6kW |
| Body Material | Double-layer Stainless Steel | |||||||
| handling capacity | 4-6m³ | 4-6m³ | 6-8m³ | 8-10m³ | 10-12m³ | 12-14m³ | 16-19m³ | 20-24m³ |
| Tip:The Moisture Content of Fresh Chicken Manure is 65-70% | ||||||||
Working principle model

Product Principle Details
Stage 1 – Heating: Raw material is put into the tank, and the oxygen supply system continuously injects oxygen. Naturally occurring bacteria and fungi multiply, decomposing organic matter and raising the temperature to around 65°C in a short time.
Stage 2 – Constant Temperature: The temperature is maintained at 45–70°C. Microorganisms efficiently decompose organic matter, while the high-temperature environment inactivates pathogens, eggs, and weed seeds, achieving harmless treatment.
Stage 3 – Cooling: After fermentation, the cooling stage begins and material is discharged. The end product is a powdered organic fertilizer with 25–30% moisture content, ready for packaging and sale.
Why choose us ?
Leading technology innovation – our professional R&D team focuses on fermentation advancements, keeping your equipment highly productive and efficient.
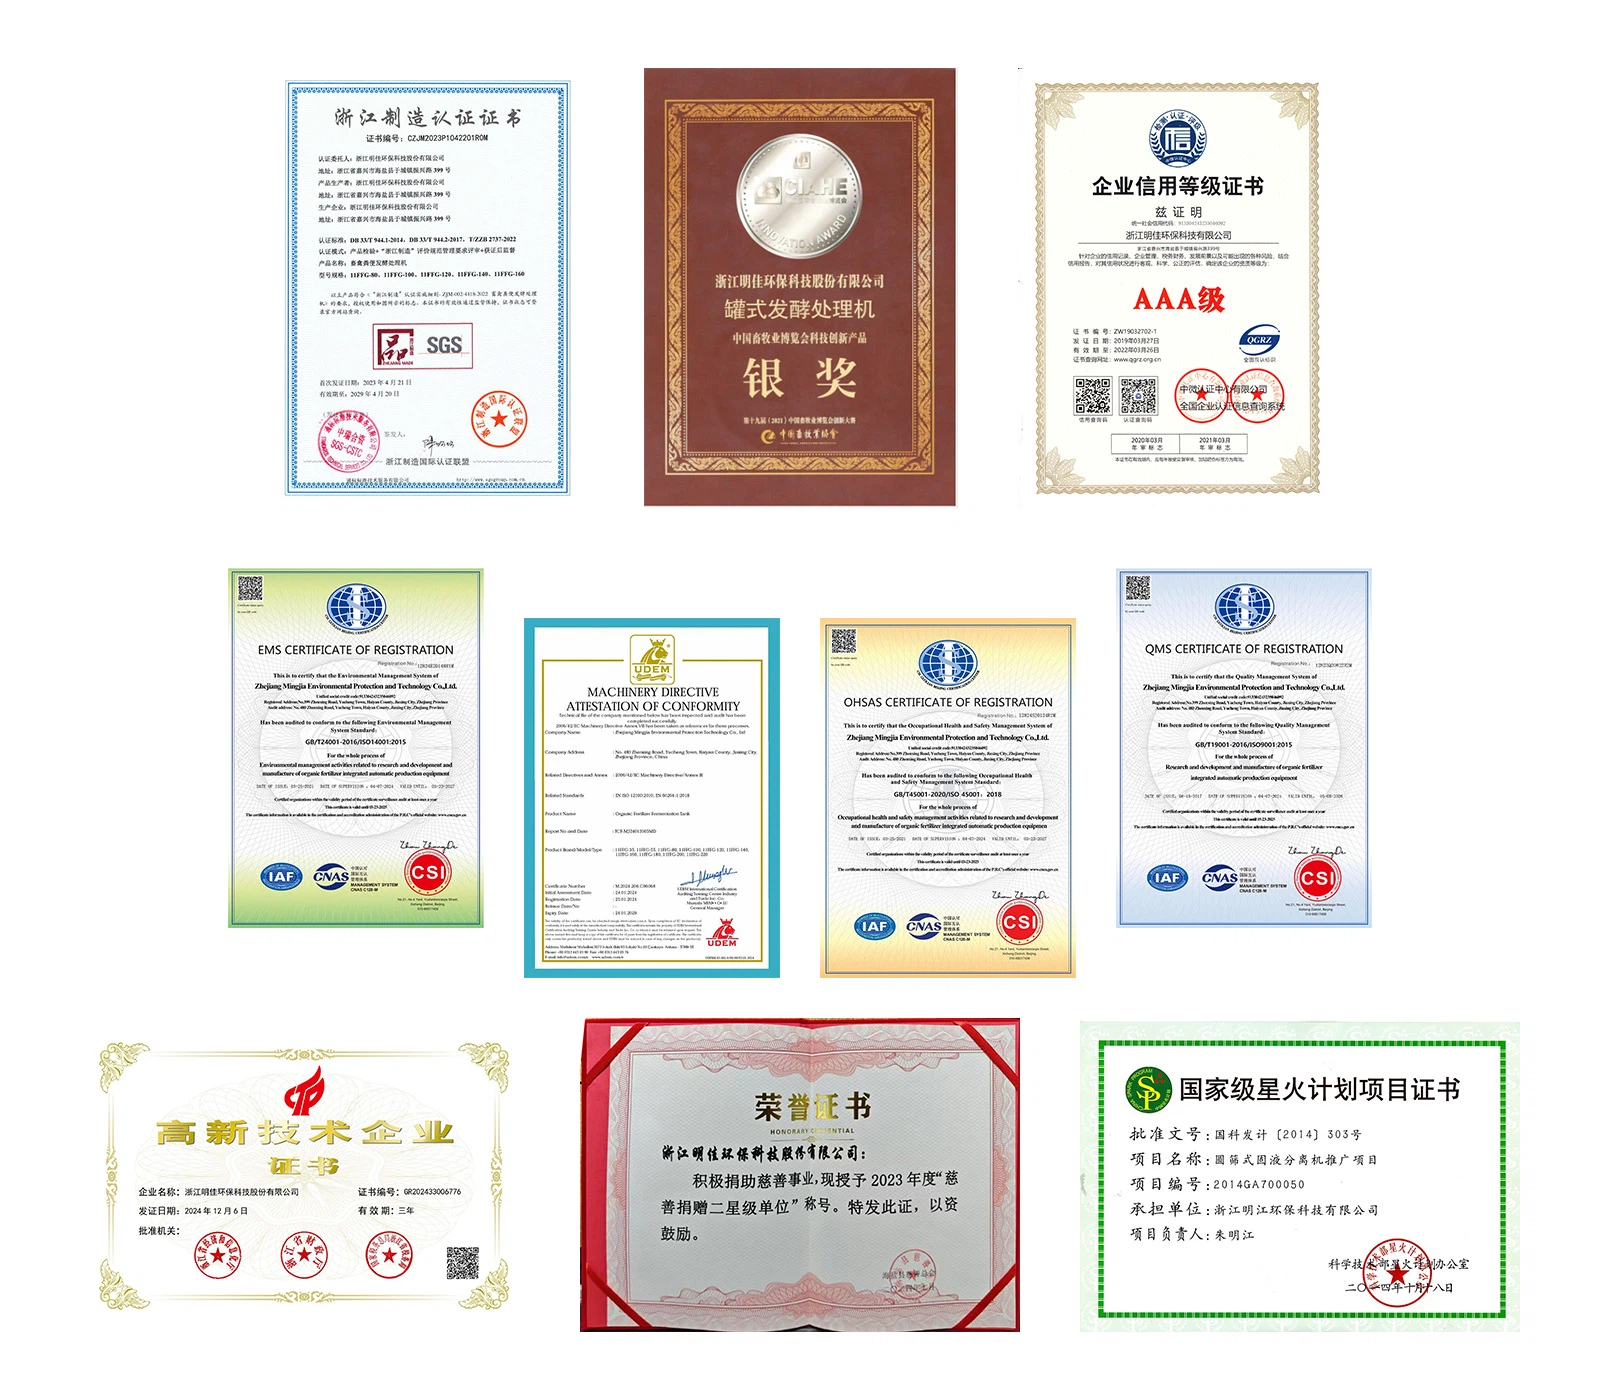
Certified industrial quality – manufactured to industrial standards, every unit undergoes strict pre-shipment testing. Certified with ISO9001, CE, and SGS.
Tailored production solutions – we customize tank specifications, capacity, and control systems based on your site scale, feedstock type, and output targets.
Complete in-house service – covering design, production, installation, commissioning, maintenance, and training – all from one supplier.
Worldwide after-sales network – service centers in Europe, Southeast Asia, and Africa offer round-the-clock technical support and spare parts delivery, cutting downtime.
Applications



Certification
Cooperation Cases


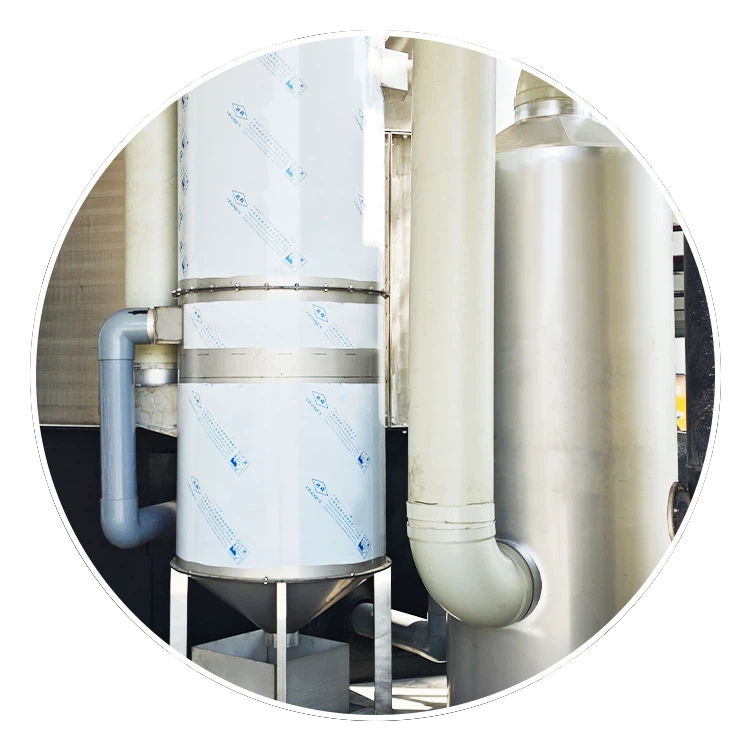
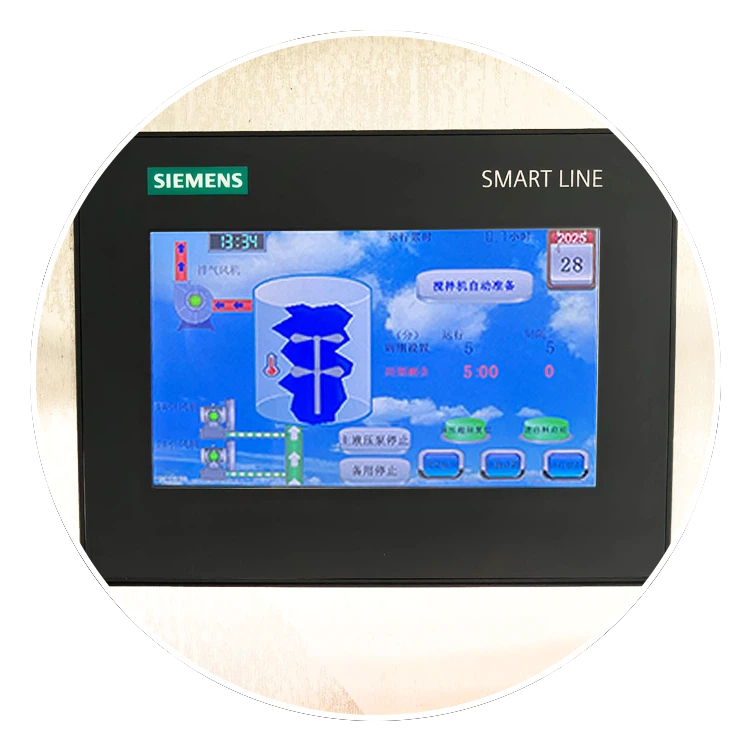
Features


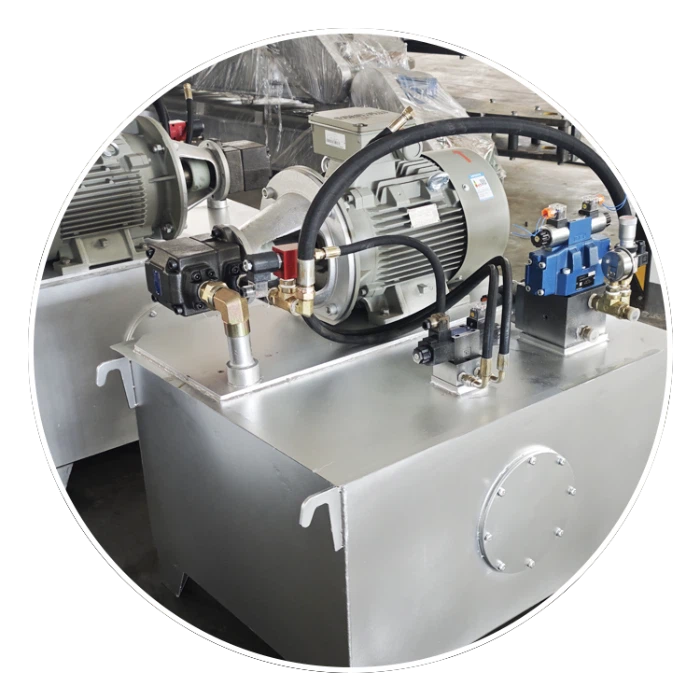
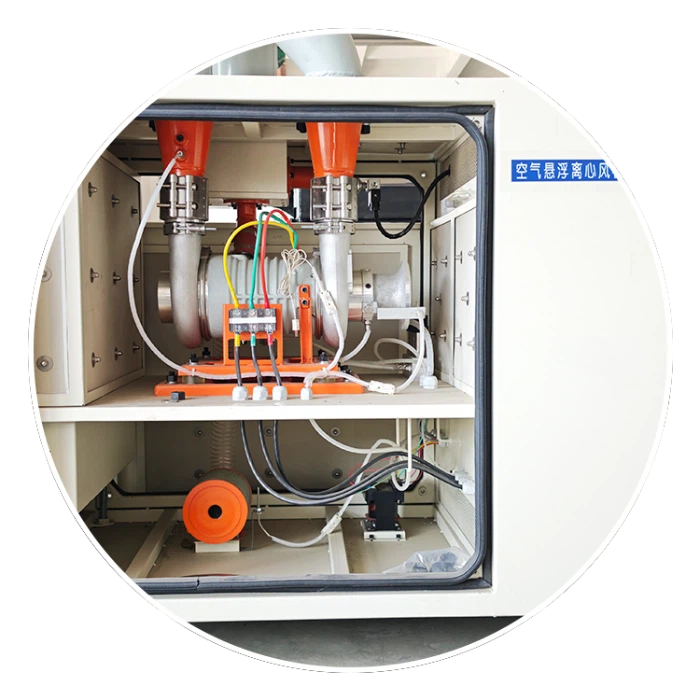
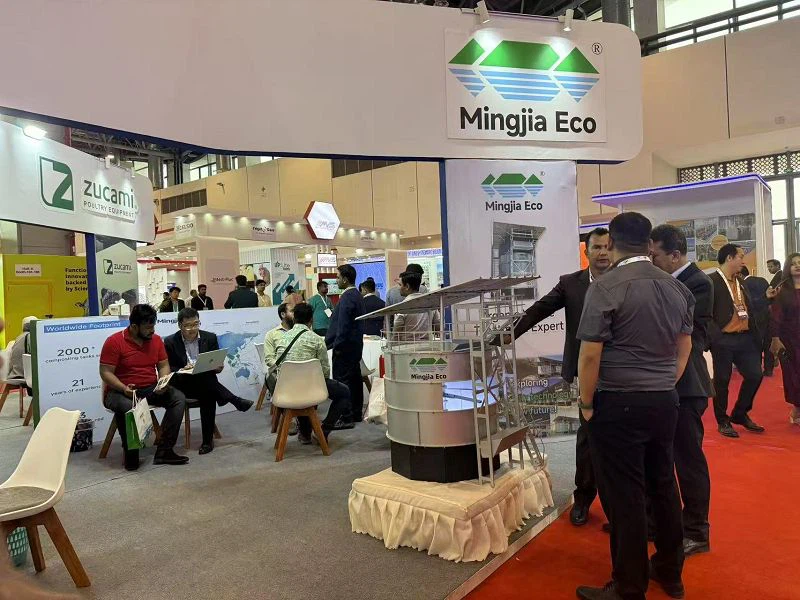
Exhibition

Shipment

Hot Tags: fully enclosed deodorizing aerobic fermentation tank, China fully enclosed deodorizing aerobic fermentation tank manufacturers, suppliers, 5 bbl fermenter, 500 liter fermentation tank, cylindrical conical tank, fermentation vessel, jacketed unitank, primary fermentation vessel


