


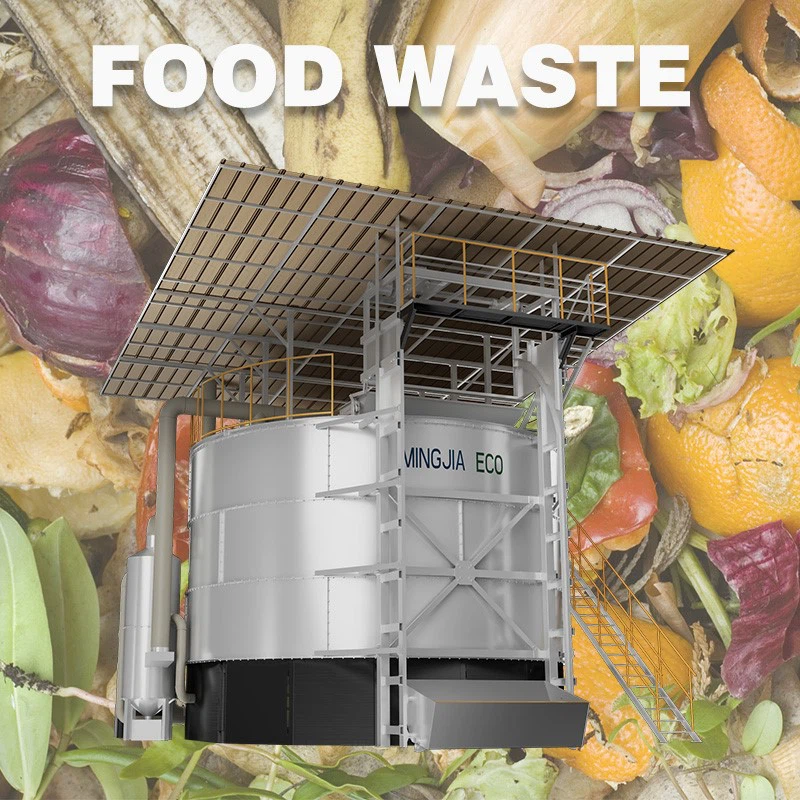
The Mingjia aerobic fermentation tank is designed specifically for egg layer manure management. In 7–10 days at 55–70°C, it converts fresh layer manure (with high moisture and ammonia content) into stable, odorless, nutrient-rich organic fertilizer at ~30% moisture. The process effectively kills Salmonella, E. coli, parasites, and weed seeds. The fully enclosed design prevents ammonia and odor release, improving farm working conditions. The finished fertilizer can be bagged or land-applied, creating additional revenue for poultry operations. The system runs 24/7 with automatic feed-in and discharge.
Models
| Model | 11FFG-55 | 11FFG-80 | 11FFG-100 | 11FFG-120 | 11FFG-140 | 11FFG-160 | 11FFG-220 | 11FFG-280 |
| Body Volume | 55m³ | 80m³ | 100m³ | 120m³ | 140m³ | 160m³ | 220m³ | 280m³ |
| Power | 29.25kW | 34.25kW | 39.25kW | 39.25kW | 43.75kW | 43.75kW | 84.25kW | 109.6kW |
| Body Material | Double-layer Stainless Steel | |||||||
| handling capacity | 4-6m³ | 4-6m³ | 6-8m³ | 8-10m³ | 10-12m³ | 12-14m³ | 16-19m³ | 20-24m³ |
| Tip:The Moisture Content of Fresh Chicken Manure is 65-70% | ||||||||
Working principle model

Efficient Fermentation & Comprehensive Harmless Treatment
The system utilizes advanced aerobic fermentation technology and an intelligent temperature control system, rapidly heating the tank interior to 55–70℃. In 7–10 days, it effectively destroys harmful bacteria, insect eggs, weed seeds, and other hazardous substances in poultry manure, while completing decomposition and maturation. The treatment cycle is 60%–80% shorter than traditional composting methods, greatly improving waste treatment efficiency.
Through high-temperature aerobic fermentation, organic matter in poultry manure is fully decomposed and transformed. Harmful components such as pathogenic microorganisms, heavy metals (effectively fixed), and odors are effectively removed. The final product meets national harmless treatment standards, preventing secondary pollution to soil, water, and air.
Why Choose Us ?
1.Leading fermentation R&D – our professional team keeps your equipment at the cutting edge of productivity and efficiency.
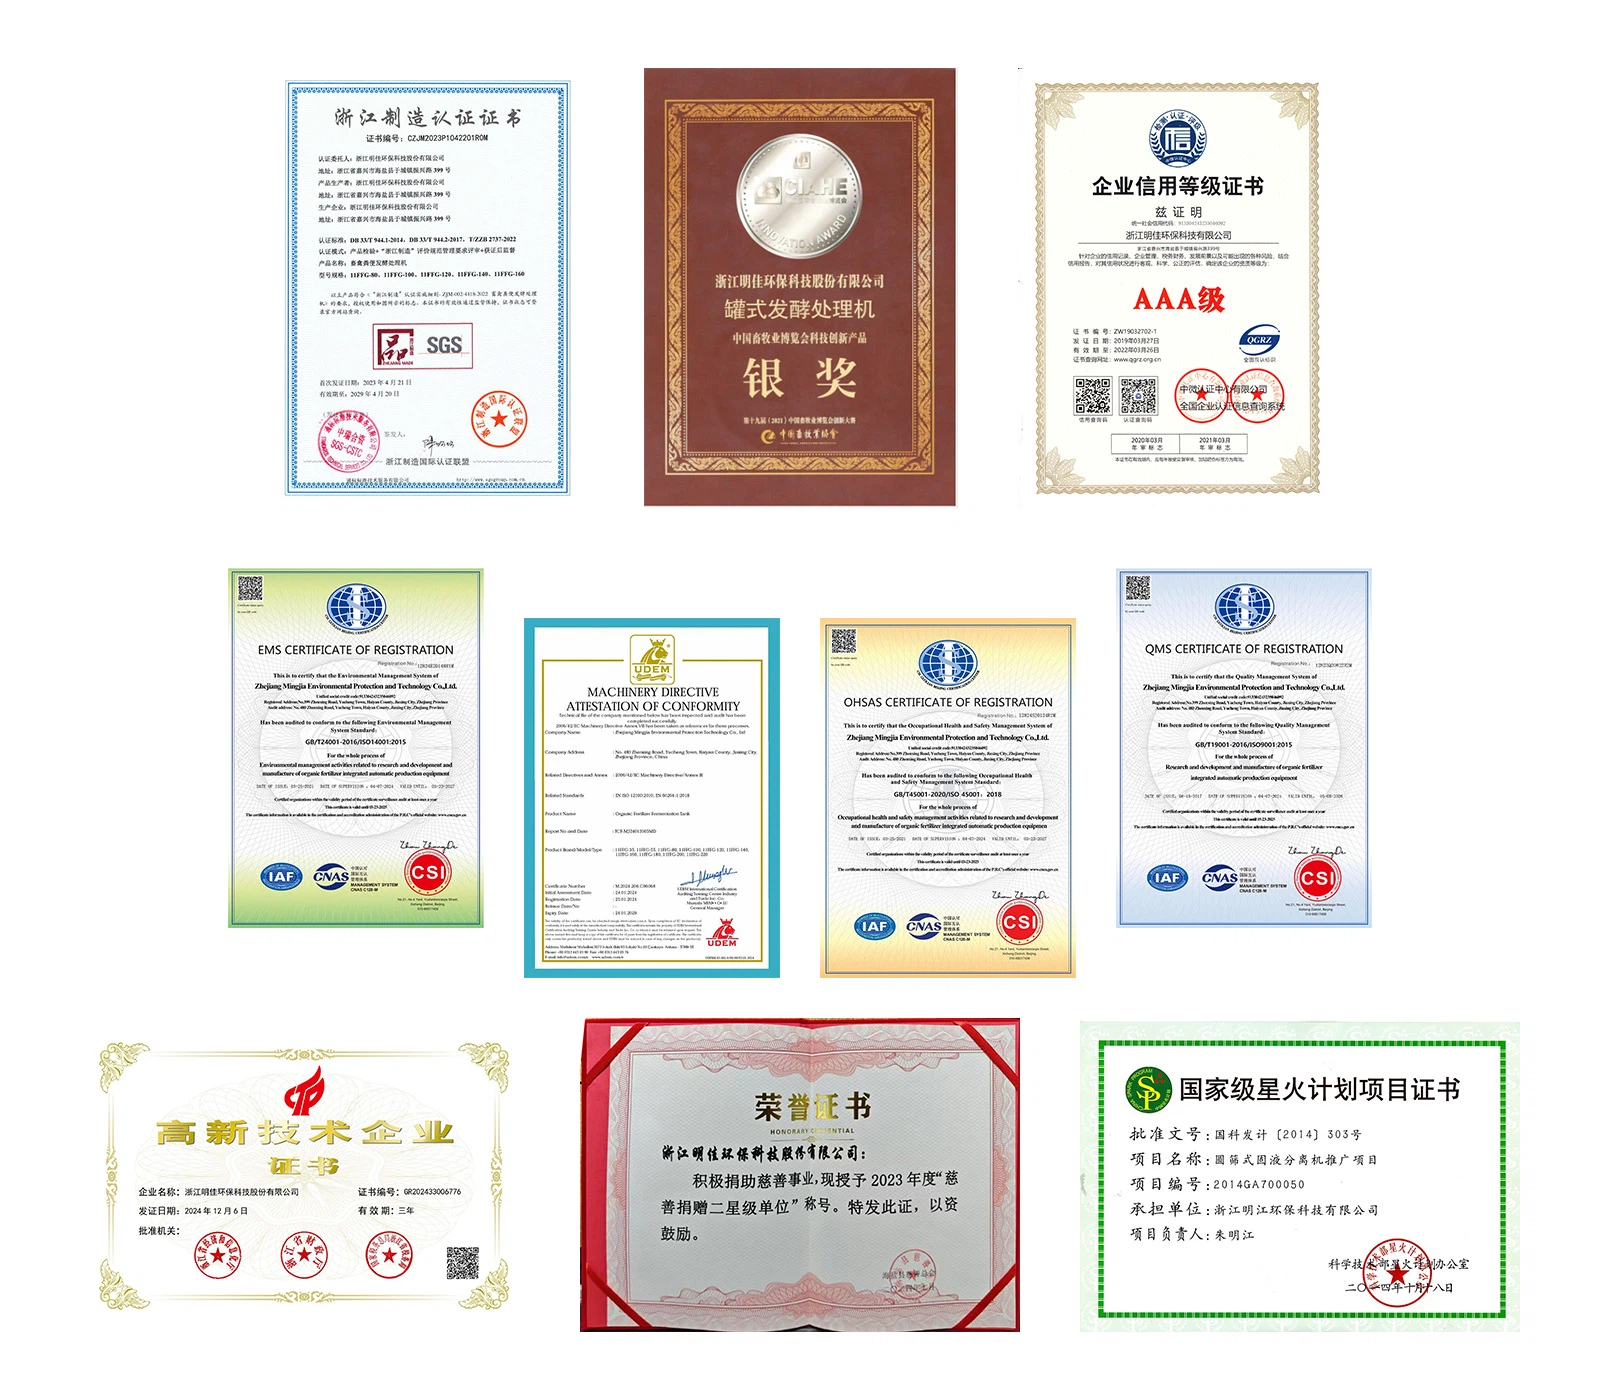
2.Industrial-grade certification – built to industrial standards, tested before shipment, and certified ISO9001, CE, and SGS.
3.Custom-tailored production solutions – we design tank size, volume, and control systems to match your plant's capacity, material type, and throughput goals.
4.One-stop service from factory – we provide full-process support: design, manufacturing, installation, commissioning, after-sales, and training.
5.Global after-sales network – service centers across Europe, Southeast Asia, and Africa deliver 24/7 technical support and spare parts, minimizing downtime.
Applications



Certification
Cooperation cases


Features


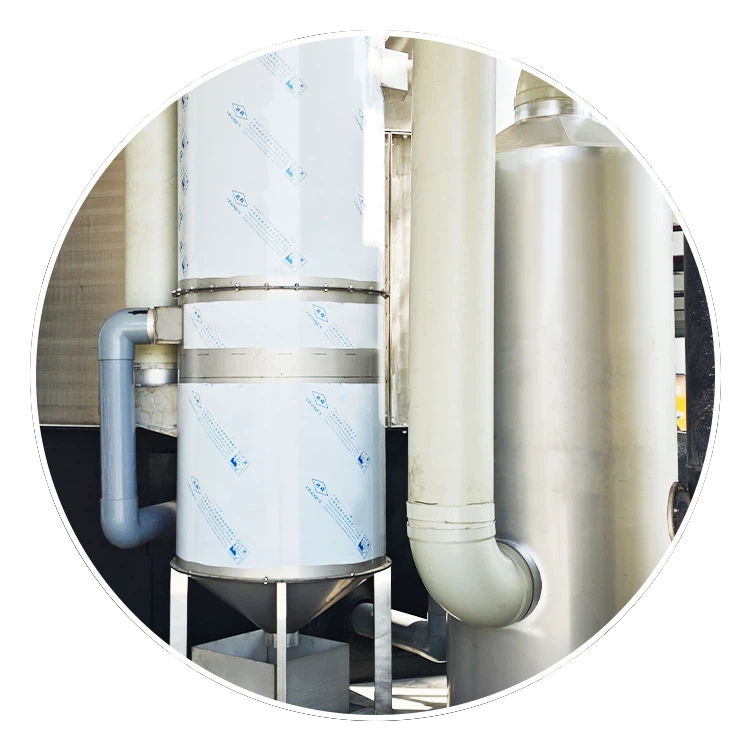
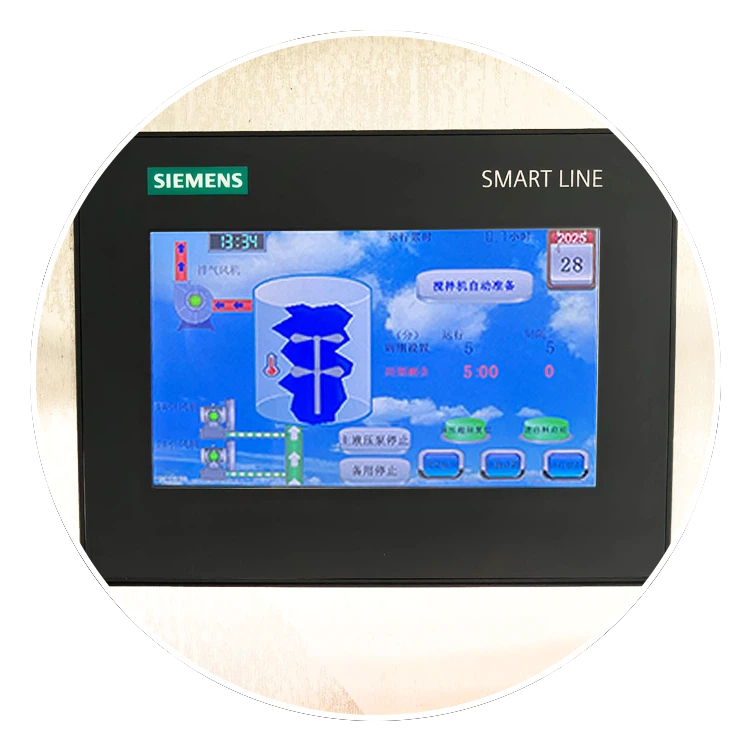
Exhibition

Shipment

Hot Tags: organic fertilizer fermentation tank for poultry farm waste / egg layer manure management, China organic fertilizer fermentation tank for poultry farm waste / egg layer manure management manufacturers, suppliers, 200l stainless steel fermenter, 25l fermentation vessel, 5 bbl unitank, 500l fermenter, cylindrical conical tank, Organic Waste Fermentation Tank


