


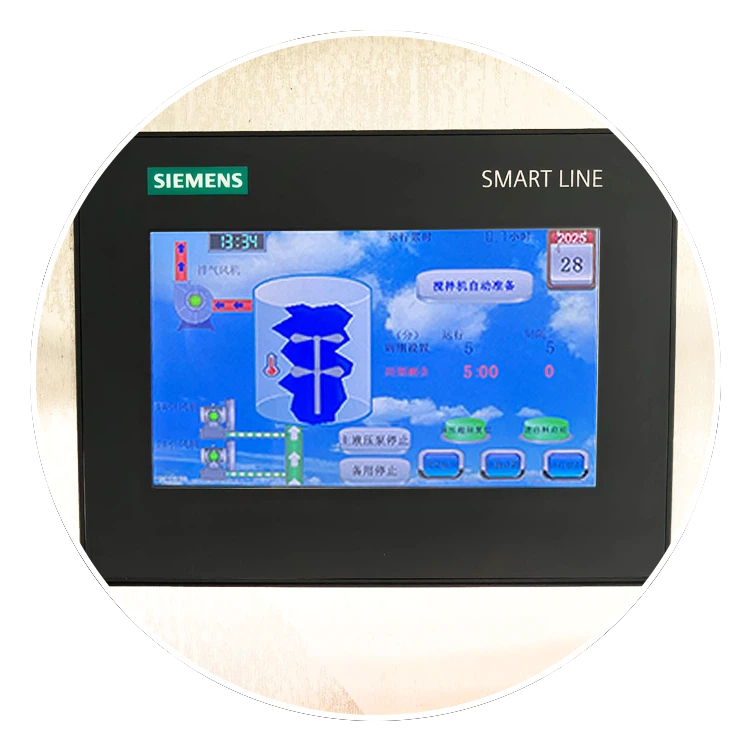
The Mingjia aerobic fermentation tank is an automatic vertical composter designed for pig manure and agricultural residue recycling. It processes swine manure, corn stalks, rice husks, and other crop residues via high-temperature aerobic fermentation. Within 7–10 days, the system converts the mixture into a stable, nutrient-balanced organic fertilizer with moisture reduced to ~30%. An intelligent control system automates feeding, mixing, aeration, and discharge, requiring minimal manual labor. The sealed structure eliminates odors and prevents groundwater pollution. The final product can be field-applied or bagged, creating a circular economy between livestock and crop farming. Ideal for medium to large-scale pig farms.
Models
| Model | 11FFG-55 | 11FFG-80 | 11FFG-100 | 11FFG-120 | 11FFG-140 | 11FFG-160 | 11FFG-220 | 11FFG-280 |
| Body Volume | 55m³ | 80m³ | 100m³ | 120m³ | 140m³ | 160m³ | 220m³ | 280m³ |
| Power | 29.25kW | 34.25kW | 39.25kW | 39.25kW | 43.75kW | 43.75kW | 84.25kW | 109.6kW |
| Body Material | Double-layer Stainless Steel | |||||||
| handling capacity | 4-6m³ | 4-6m³ | 6-8m³ | 8-10m³ | 10-12m³ | 12-14m³ | 16-19m³ | 20-24m³ |
| Tip:The Moisture Content of Fresh Chicken Manure is 65-70% | ||||||||
Working principle model

Product Principle Details
Stage 1 – Heating: After raw materials are loaded into the tank, the oxygen supply system continuously blows in oxygen. Naturally occurring bacteria, fungi, and actinomycetes multiply rapidly in this oxygen-rich environment and quickly decompose organic matter. The material then heats up naturally to around 65°C within a short time.
Stage 2 – Constant Temperature: The equipment enters the constant temperature stage, with the internal temperature maintained between 45°C and 70°C. Microorganisms continue to work efficiently, fully breaking down the organic matter. Meanwhile, the high temperature kills pathogens, insect eggs, and weed seeds, achieving harmless treatment.
Stage 3 – Cooling: After fermentation is complete, the cooling stage begins, and the material is discharged through the outlet. The final product is a powdered organic fertilizer with about 25%–30% moisture content, rich in nutrients and ready to be packed and sold directly.
Tank Features
I. Sealed Design & High-temperature Sterilization
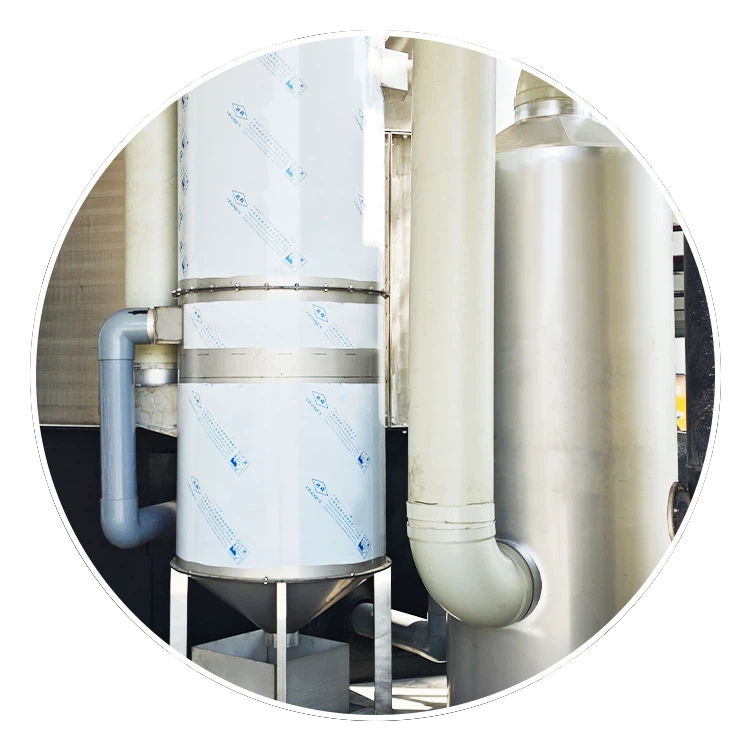
Sealed Design – The fermentation occurs in a closed space, effectively controlling odor release and preventing mosquito and fly infestation, thus reducing impact on the surroundings.
High-temperature Sterilization & Uniform Mixing – The tank temperature reaches 60–70°C, destroying harmful bacteria, insect eggs, and weed seeds for safe fertilizer. Even mixing and aeration ensure thorough decomposition, reducing organic acids and other harmful substances while improving fertilizer quality.
II. Stainless Steel Structure & Forged Ratchet
Stainless Steel Inner & Outer Tank – Made from a single thick stainless plate, providing superior corrosion resistance, sealing, and durability compared to common single-layer or welded tanks.
Forged Integral Ratchet – The forging process yields a weld-free, compact component with higher sealing integrity, greater load capacity, and a significantly lower failure rate, prolonging equipment life.

Applications


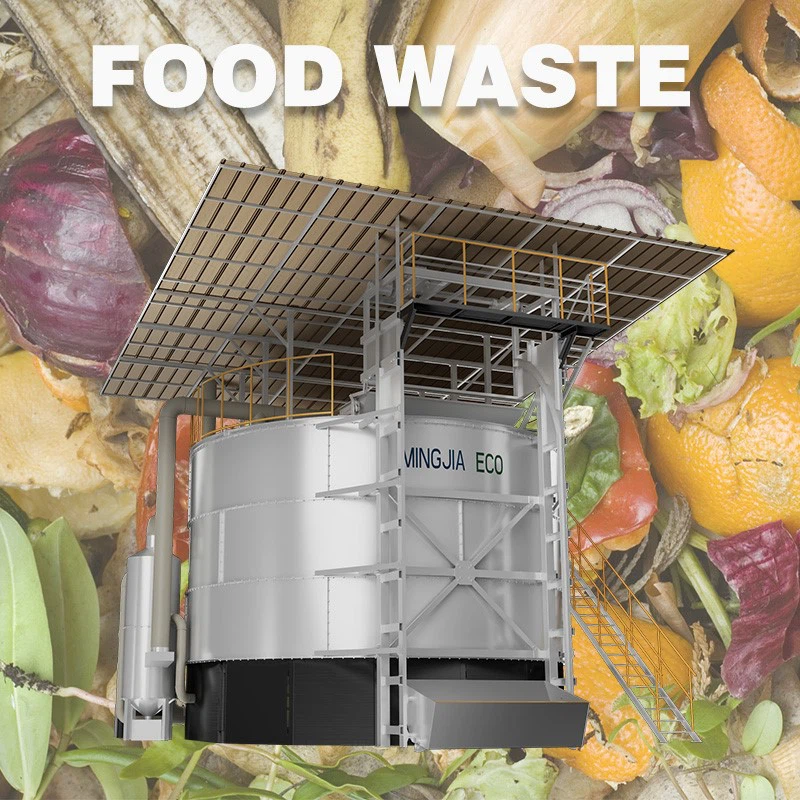

Certification
Cooperation cases


Features


Exhibition

Shipment

Hot Tags: automatic aerobic compost tower for pig farm manure and agricultural residues recycling, China automatic aerobic compost tower for pig farm manure and agricultural residues recycling manufacturers, suppliers, 5000l fermenter, 60 bbl fermenter, 7 bbl conical fermenter, Aerobic Compost Tank, Poultry Farm Composter, tank fermentation


