


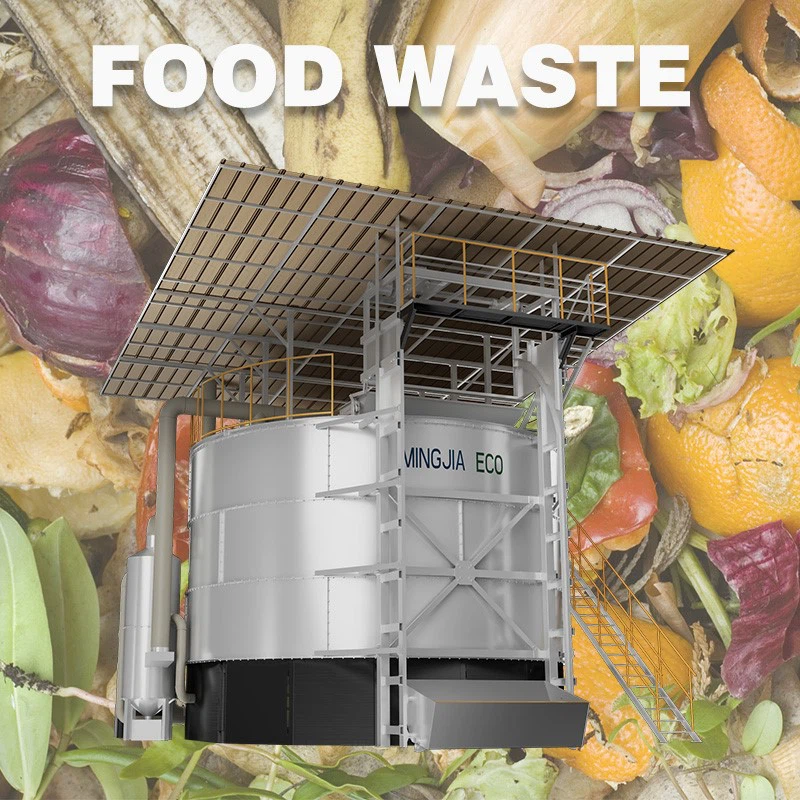
Organic waste from poultry, livestock, and municipal sources is often seen as a costly problem. Mingjia sees it as an opportunity. Our aerobic fermentation tank processes manure, kitchen waste, and sludge into premium organic fertilizer in just 7–10 days. The resulting compost enriches soil, reduces the need for chemical fertilizers, and creates a closed-loop system where waste feeds the earth. Effective, economical, and eco-friendly.
Models
| Model | 11FFG-55 | 11FFG-80 | 11FFG-100 | 11FFG-120 | 11FFG-140 | 11FFG-160 | 11FFG-220 | 11FFG-280 |
| Body Volume | 55m³ | 80m³ | 100m³ | 120m³ | 140m³ | 160m³ | 220m³ | 280m³ |
| Power | 29.25kW | 34.25kW | 39.25kW | 39.25kW | 43.75kW | 43.75kW | 84.25kW | 109.6kW |
| Body Material | Double-layer Stainless Steel | |||||||
| handling capacity | 4-6m³ | 4-6m³ | 6-8m³ | 8-10m³ | 10-12m³ | 12-14m³ | 16-19m³ | 20-24m³ |
| Tip:The Moisture Content of Fresh Chicken Manure is 65-70% | ||||||||
Working principle model

Product Principle Details
Stage 1 – Heating: When raw material enters the tank, the air supply system continuously blows in oxygen. Naturally occurring bacteria, fungi, and actinomycetes multiply rapidly in this oxygen-rich environment and quickly decompose organic matter. As a result, the material naturally heats up to around 65°C in a short time.
Stage 2 – Constant Temperature: The system then enters a constant temperature stage, maintaining an internal temperature of 45–70°C. Microorganisms continue to work efficiently, fully breaking down the organic matter. At the same time, the high temperature kills pathogens, insect eggs, and weed seeds, achieving harmless treatment.
Stage 3 – Cooling: After fermentation is complete, the cooling stage begins, and the material is discharged through the outlet. The final product is a powdered organic fertilizer with about 25%–30% moisture content, rich in nutrients and ready to be packed and sold directly.
Tank Features
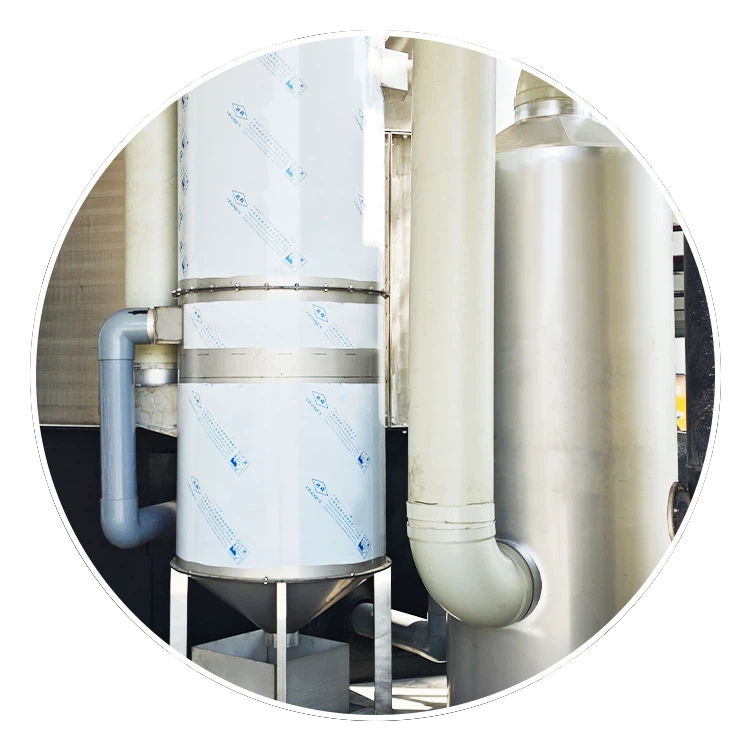
Stainless steel double-layer tank – Two layers of corrosion-resistant stainless steel, large capacity (several to hundreds of cubic meters), fully sealed to prevent odor leakage.
High-temperature sterilization & sealed design – 60–70°C kills pathogens, eggs, and weed seeds; sealed structure blocks odors and insects.
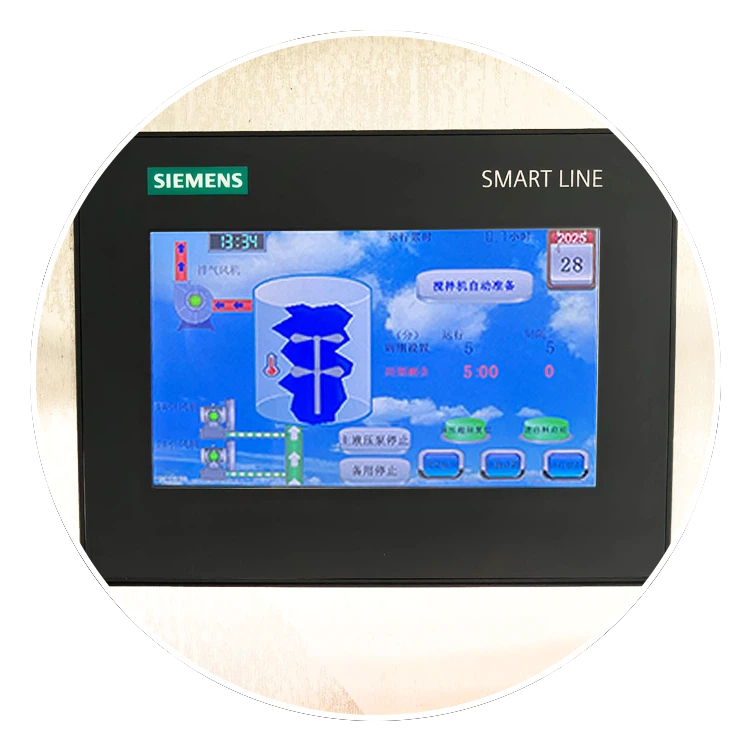
Mixing system – Mechanical agitators with proper power ensure uniform mixing for higher fermentation efficiency.
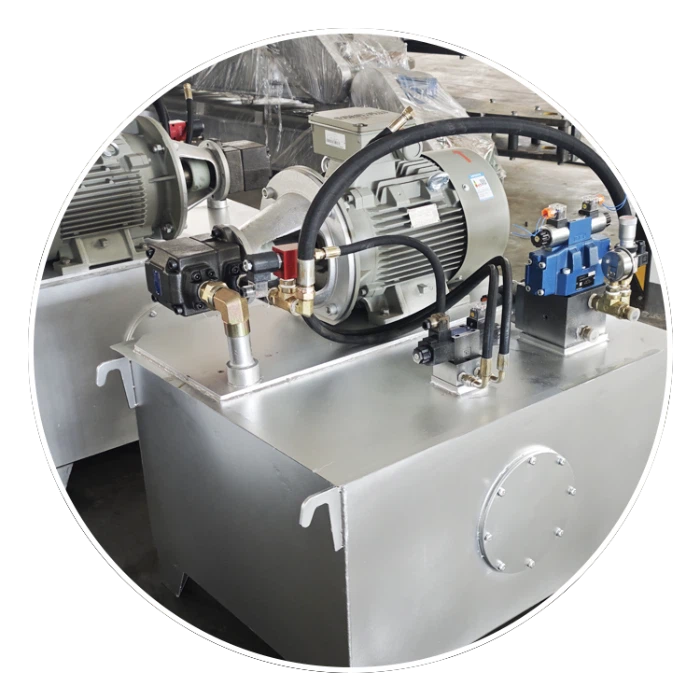
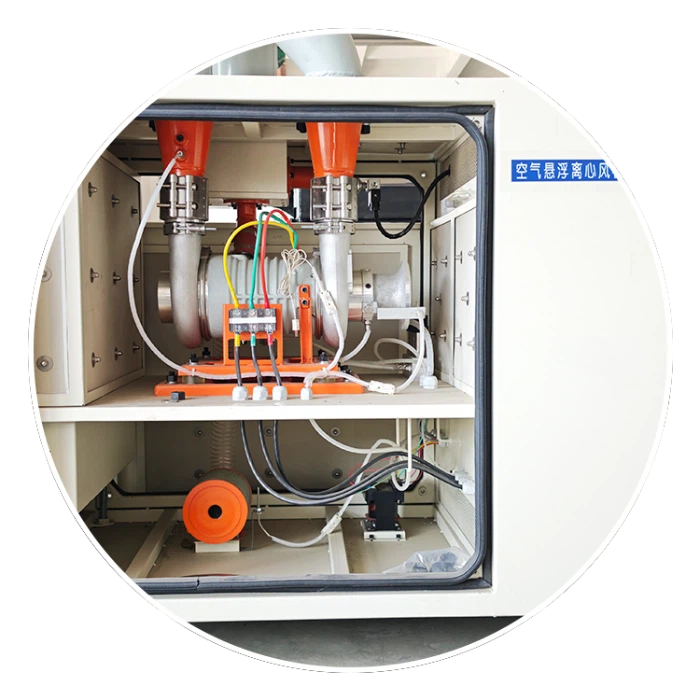
Aeration system – Air blowers and pipelines supply fresh oxygen, essential for organic matter decomposition and stable compost production.
Forged ratchet & insulation – Weld-free forged ratchet offers high load capacity and low failure rate; high-density polyurethane foam provides excellent heat retention.

Applications



Certification

Cooperation cases


Features


Exhibition

Shipment

Hot Tags: poultry and livestock farm automatic fermentation tank high productivity manure to fertilizer machine, China poultry and livestock farm automatic fermentation tank high productivity manure to fertilizer machine manufacturers, suppliers, 100 bbl fermenter, 20 bbl conical fermenter, 20 gallon fermentation tank, 500 gallon fermentation tank, 7 bbl unitank, Chicken Manure Fertilizer Compost


